Raw Material Premix control (291-MY1) using CB-OMNI
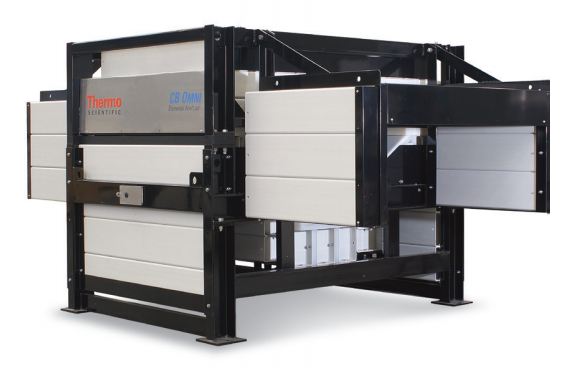
The online analyzer is being installed to monitor and control the premix comprising of Limestone, Tuff and weathered Siltstone. These materials are fed through weigh feeders onto a common crusher. The average particle size in the premix will be 95% passing 100mm or lower and will be fed onto a 1000mm belt 291-BC1 at a nominal throughput of 815tph travelling at 2m/sec belt speed. The proposed analyzer will be installed on this belt that will be carrying this premix.
In order to achieve an efficient kiln operation with a consistent quality product, it is essential to have target quality of kiln feed consistently. To be able to accomplish this goal:
- The proportions of the various raw materials need to be dynamically controlled based on actual chemistry and the desired quality target.
- The system should operate with minimum manual intervention.
With the incorporation of the analyzer into the process, the real time monitoring of the raw mix and high frequency process control will proceed as follows:
+ The real time measurement will provide minute-to-minute analysis of the raw mix in terms of SiO2, Al2O3, Fe2O3, CaO, SO3, MgO, K2O, and Na2O that will be displayed on the OPCON operator interface.
+ The base software also has the capability to compute quality control parameters such as LSF, Silica Modulus, Aluminum Ratio, C3S, C3A, etc. using the real time oxide information as measured.
+ The control software PREBOS Plus then compares the real time quality target as measured versus that required by the application.
+ PREBOS Plus then provides optimum blend proportions of raw mix in order to meet the quality control targets of the kiln feed.
+ Feedback from the optional control software will be directed to the plant PLC network to implement the corrective actions to proportion the raw material feed rates.
Advantages of On-line analyzer based raw mix control:
1. As full flow of material is analyzed continuously, there is no sampling or sample preparation error.
2. The entire operation being a continuous process calls for a high frequency control devoid of human intervention, sampling and other operations
3. Improved homogeneity.
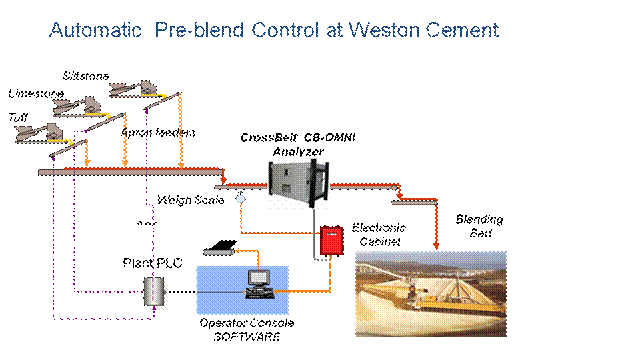
Typical flow scheme for premix control using CB-OMNI Analyzer
Note: The schematic diagram shown is typical and based on the brief understanding of customer’s application by the author of this proposal. Actual site conditions and associated equipment may vary. The diagram depiction is only to give the customer a brief idea of the control logic and process control possibilities.
Mill Feed control (331-MY1) using CB-OMNI
The online analyzer is being installed to monitor and control the mill feed comprising of the premix (Limestone, Tuff and weathered Siltstone mixture), Corrective Limestone, Bauxite and Sand. These materials are fed through individual weigh feeders onto a common belt. The average particle size in the premix will be 95% passing 100mm or lower and will be fed onto a 1000mm belt 331-BC1 at a nominal throughput of 390tph travelling at 1.5m/sec belt speed. The proposed analyzer will be installed on this belt that will be seeing a layered mixture of the above mentioned materials.
The belt loading is lower than the nominal loading of 125kg/m required for a 1000mm belt. It is recommended that the belt is slowed down to around 0.8m/sec to achieve this as well as a suitable installation position be sought to avoid the layering if possible.
In order to achieve an efficient kiln operation with a consistent quality product, it is essential to have target quality of kiln feed consistently. To be able to accomplish this goal:
- The proportions of the various raw materials need to be dynamically controlled based on actual chemistry and the desired quality target.
- The system should operate with minimum manual intervention.
With the incorporation of the analyzer into the process, the real time monitoring of the raw mix and high frequency process control will proceed as follows:
+ The real time measurement will provide minute-to-minute analysis of the raw mix in terms of SiO2, Al2O3, Fe2O3, CaO, SO3, MgO, K2O, and Na2O that will be displayed on the OPCON operator interface.
+ The base software also has the capability to compute quality control parameters such as LSF, Silica Modulus, Aluminum Ratio, C3S, C3A, etc. using the real time oxide information as measured.
+ The control software RAMOS then compares the real time quality target as measured versus that required by the application.
+ RAMOS then provides optimum blend proportions of raw mix in order to meet the quality control targets of the kiln feed.
+ Feedback from the optional control software will be directed to the plant PLC network to implement the corrective actions to proportion the raw material feed rates
Advantages of On-line analyzer based mill-feed control:
4. As full flow of material is analyzed continuously, there is no sampling or sample preparation error.
5. The entire operation being a continuous process calls for a high frequency control devoid of human intervention, sampling and other operations
6. Improved homogeneity.
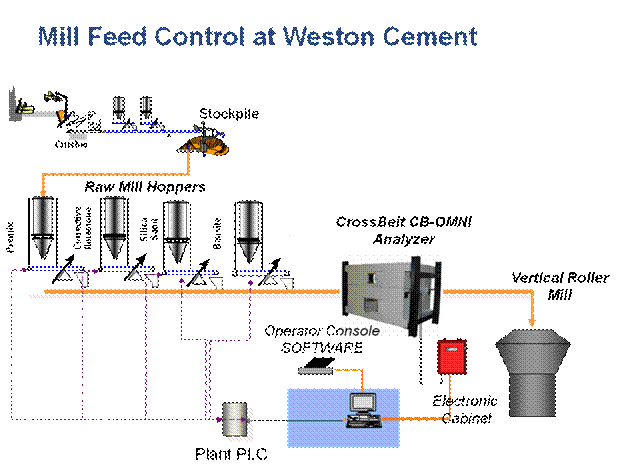
Typical flow scheme for mill feed control using CB-OMNI Analyzer
Note: The schematic diagram shown is typical and based on the brief understanding of customer’s application by the author of this proposal. Actual site conditions and associated equipment may vary. The diagram depiction is only to give the customer a brief idea of the control logic and process control possibilities. |




.jpg "Calcium")